Enhancing Product Safety: The Role of Packing Machines in Milk Quality Control
Date:
2025-05-30
Enhancing Product Safety: The Role of Packing Machines in Milk Quality Control
Table of Contents
- Introduction: The Importance of Milk Quality Control
- Understanding Packing Machines in the Dairy Industry
- Technologies Used in Modern Packing Machines
- Quality Control Measures in Packing Machines
- Benefits of Advanced Packing Machines for Product Safety
- Case Studies: Real-World Applications
- Future Trends in Packing Machines and Milk Quality Control
- Conclusion: Ensuring Safety Through Innovation
- FAQs
Introduction: The Importance of Milk Quality Control
In the dairy industry, ensuring **milk quality** is critical not only for consumer health but also for brand reputation. The rise of **advanced packing machines** has significantly enhanced product safety protocols, enabling dairy manufacturers to maintain the integrity of their products from processing through to packaging. As consumers become increasingly health-conscious, understanding the mechanisms behind milk quality control becomes essential.
Understanding Packing Machines in the Dairy Industry
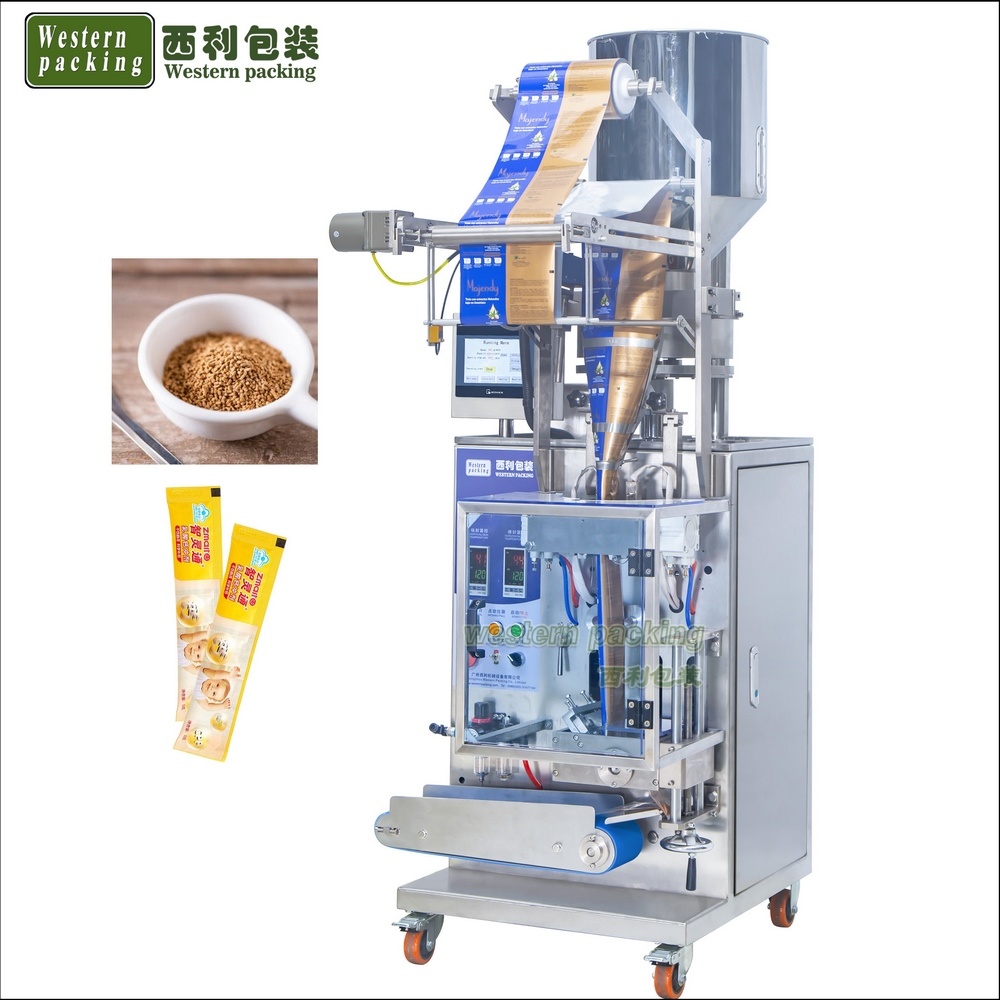
Packing machines play a crucial role in the dairy sector. These machines are designed to efficiently package milk and milk products while preserving quality. In an industry where contamination can lead to severe health risks, investing in reliable packing technology is paramount.
The Role of Automation
Automation within packing machines allows for consistent and precise filling, capping, and sealing processes. This reduces the risk of human error, which can compromise the safety of milk products. Automated systems can also integrate with **quality assurance technologies**, providing real-time feedback and adjustments throughout the packing process.
Types of Packing Machines
Different types of packing machines are utilized in the dairy industry, including:
- **Liquid Filling Machines**: Specifically designed for various milk forms, ensuring accurate volumes.
- **Capping Machines**: Sealing packages to avoid contamination and leakage.
- **Labeling Machines**: Ensuring that all compliance information is correctly displayed on the packaging.
Technologies Used in Modern Packing Machines
Modern packing machines incorporate cutting-edge technology to enhance milk quality control further.
Smart Sensors and IoT Integration
The integration of smart sensors allows for continuous monitoring of critical parameters such as:
- Temperature
- Humidity
- Fill levels
These sensors provide invaluable data, enabling manufacturers to make informed decisions regarding production and packaging conditions.
Advanced Sealing Technologies
Modern sealing techniques, including vacuum sealing and modified atmosphere packaging, help extend the shelf life of milk. These methods reduce the oxygen level within the packaging, minimizing the growth of spoilage microorganisms and maintaining freshness.
Quality Control Measures in Packing Machines
Quality control within packing machines is vital for maintaining the high standards expected in milk production.
Regular Maintenance and Calibration
Routine maintenance and calibration of packing machines ensure they operate within specified parameters. Regular checks help to identify wear and tear, preventing potential malfunctions that could compromise product safety.
Compliance with Industry Standards
Packing machines must comply with various industry regulations, such as the FDA and USDA standards. Adhering to these regulations ensures that all safety protocols are met, thereby protecting consumers.
Benefits of Advanced Packing Machines for Product Safety
The use of advanced packing machines brings numerous advantages, particularly concerning product safety.
Enhanced Freshness and Shelf Life
By effectively sealing products and preventing contamination, advanced packing machines extend the **shelf life** of milk. This not only meets consumer demands for freshness but also reduces food waste.
Improved Traceability
Modern packing solutions often include barcode or QR code systems that enhance traceability. This enables manufacturers to track products throughout the supply chain, facilitating swift action in case of recalls.
Case Studies: Real-World Applications
Understanding real-world applications provides insight into the effectiveness of advanced packing machines in maintaining milk quality.
Case Study 1: XYZ Dairy
XYZ Dairy implemented a fully automated packing line equipped with IoT sensors that monitor temperature and humidity. This system reduced spoilage rates by 30%, ensuring customers received fresher products.
Case Study 2: ABC Farms
ABC Farms adopted vacuum sealing technology for its milk products. The result was a 25% increase in shelf life, leading to higher customer satisfaction and lower returns.
Future Trends in Packing Machines and Milk Quality Control
The future of packing machines in relation to milk quality control promises exciting innovations.
AI and Machine Learning
The incorporation of AI and machine learning algorithms will allow for predictive maintenance, enhancing efficiency and reducing downtime. These technologies will enable packing machines to learn from previous data, optimizing packaging processes over time.
Sustainability Initiatives
As sustainability becomes a priority, manufacturers will look for eco-friendly packaging solutions. Innovations in biodegradable and recyclable materials will likely reshape the packaging landscape in the dairy sector.
Conclusion: Ensuring Safety Through Innovation
The role of packing machines in milk quality control cannot be overstated. By leveraging cutting-edge technology, manufacturers can ensure the safety and integrity of their products, meeting consumer expectations for freshness and quality. Continuous advancements in packing technology will further enhance product safety, reinforcing trust between consumers and dairy producers.
FAQs
1. How do packing machines improve milk safety?
Packing machines enhance milk safety by preventing contamination and ensuring proper sealing and storage conditions.
2. What types of packing machines are used for milk?
Common types include liquid filling machines, capping machines, and labeling machines.
3. How does automation benefit the packing process?
Automation reduces human error, increases efficiency, and ensures consistent packaging quality.
4. What technologies are integrated into modern packing machines?
Smart sensors, IoT integration, and advanced sealing technologies are among the key innovations.
5. Why is regular maintenance of packing machines important?
Regular maintenance ensures machines operate efficiently and comply with safety standards, reducing the risk of product spoilage or contamination.
packing machine milk

Innovations in Granule Packing Technology You Should Know
Innovations in Granule Packing Technology: A Comprehensive Guide Table of Contents Understanding Granule Packing Technology Importance of Granule Packing in Manufacturing Key Innovations in Granule Packing Technology The Role of Automation in Granule Packing Sustainable Packaging Solutions for Granules Advanced Sensors and Monitoring Systems Case Studies and Industry Examples Futu
2026-08-28
Maximize Efficiency with Advanced Tea Bag Packing Machines
In the realm of packaging machinery, tea bag packing machines represent a vital innovation for manufacturers in the tea industry. These specialized machines are designed to automate the tea bag production process, significantly increasing efficiency while maintaining the quality of the product. With the growing demand for convenient tea options, understanding the functionality and advantages of te
2026-08-27
How Food Packaging Machines Enhance Product Safety and Compliance
How Food Packaging Machines Enhance Product Safety and Compliance Table of Contents 1. Introduction to Food Packaging Machines 2. The Importance of Food Safety in Packaging 3. Types of Food Packaging Machines 4. Advanced Technologies in Food Packaging 5. Regulatory Compliance in Food Packaging 6. The Impact of Food Packaging on Product Safety 7. Best Practices for Food
2026-08-26

Head office :
112 ROBINSON ROAD #03-01 ROBINSON 112 ,SINGAPORE
HONGKONG BRANCH :
12/F ZJ 300 300 LOCKHART ROAD WAN
CHAI HK
GUANGZHOU BRANCH:
3th, Yilongjie Wulonggang, Zhongluotan, Baiyun district, Guangzhou,China
Subscribe to our newsletter and get professional packaging solution


SAF Coolest v1.3.1.2 设置面板 UFQSX-ANRV-PSSVE-XVF
无数据提示
Sorry, the current column is being updated, please look forward to it!