Efficient Solutions: The Advantages of Liquid Sachet Packing Machines
Date:
2024-08-17
Efficient Solutions: The Advantages of Liquid Sachet Packing Machines
Table of Contents
- Introduction to Liquid Sachet Packing Machines
- What Are Liquid Sachet Packing Machines?
- Key Benefits of Liquid Sachet Packing Machines
- Variety of Applications
- Technology Advancements in Liquid Sachet Packing
- Sustainability Considerations
- Choosing the Right Liquid Sachet Packing Machine
- FAQs About Liquid Sachet Packing Machines
- Conclusion
Introduction to Liquid Sachet Packing Machines
In the dynamic world of packaging, the efficiency and effectiveness of the machinery used can significantly impact a company’s bottom line. **Liquid sachet packing machines** have emerged as a transformative solution for businesses aiming to streamline their packing processes while maintaining high standards of product quality. These machines are designed to pack liquids into small pouches or sachets, offering a range of benefits that cater to various industries. As we delve deeper into this topic, we will explore the advantages these machines bring to manufacturing operations.
What Are Liquid Sachet Packing Machines?
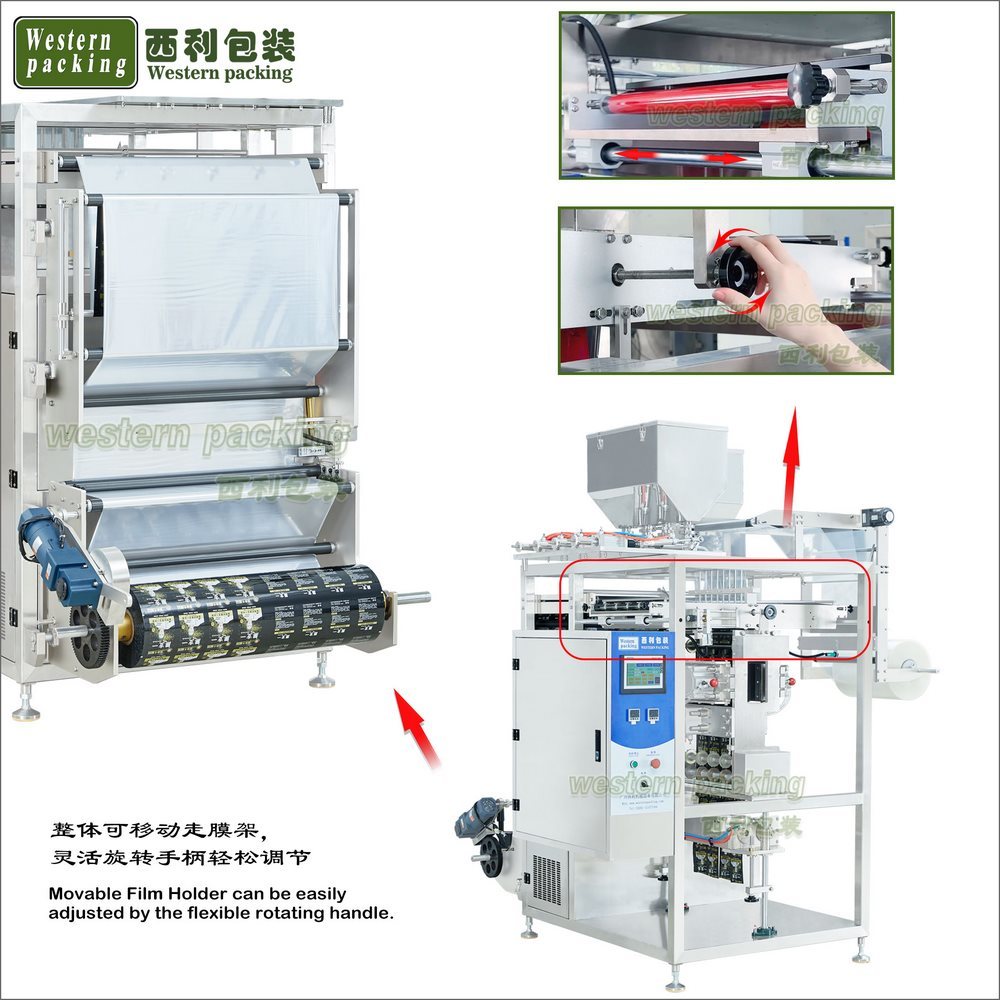
Liquid sachet packing machines are specialized devices that automate the process of filling and sealing liquid products into small, flexible packages. These machines can handle various types of liquids, including sauces, oils, beverages, and more. The packing process typically involves several critical steps:
1. **Filling**: The machine dispenses the desired volume of liquid into the sachet.
2. **Sealing**: The sachet is then sealed to ensure that the product remains fresh and uncontaminated.
3. **Cutting**: After sealing, the machine can cut the sachets to the desired size.
These machines are engineered for precision and speed, making them essential for high-volume production lines.
Key Benefits of Liquid Sachet Packing Machines
Liquid sachet packing machines offer several key benefits that significantly enhance operational efficiency. Below, we delve into three primary advantages.
Increased Efficiency in Production
One of the most significant advantages of liquid sachet packing machines is their ability to boost production efficiency. By automating the packing process, these machines reduce the time and labor required for manual packing. This automation leads to:
- **Faster Production Rates**: Modern machines can fill and seal hundreds of sachets per minute, allowing for quick turnaround times.
- **Reduced Labor Costs**: With fewer employees needed on the packing line, companies can lower their labor expenses.
- **Consistent Output Quality**: Automated systems minimize human error, ensuring that each sachet is filled and sealed uniformly.
Incorporating liquid sachet packing machines into production lines can lead to substantial improvements in overall efficiency.
Cost-Effectiveness
Investing in liquid sachet packing machines can yield significant cost savings over time. The initial investment is often recouped through the following means:
- **Lower Material Costs**: Sachets require less packaging material compared to traditional bottles or jars. This reduction in material usage translates to lower costs.
- **Minimized Product Waste**: Precise filling reduces the likelihood of overfilling, which can diminish product waste and enhance profitability.
- **Long-Term Durability**: Quality machines are built to last, requiring minimal repairs and maintenance, further driving down long-term costs.
By increasing efficiency and reducing input costs, liquid sachet packing machines create a compelling case for businesses looking to optimize their operations.
Enhanced Product Integrity
Product integrity is paramount in the packaging industry. Liquid sachet packing machines ensure that products remain uncontaminated and fresh through the following features:
- **Sealing Technology**: Advanced sealing techniques create airtight pouches, preventing leakage and spoilage.
- **Material Options**: Sachets can be made from various barrier materials that protect contents from light, moisture, and air, extending shelf life.
- **Tamper-Proof Designs**: Many machines can incorporate tamper-evident features, enhancing consumer safety and confidence.
With enhanced product integrity, businesses can assure customers of the quality and safety of their products, fostering brand loyalty.
Variety of Applications
Liquid sachet packing machines are versatile, serving diverse industries including food and beverage, cosmetics, pharmaceuticals, and more. This flexibility enables businesses to adapt to market demands effectively. Here are some common applications:
- **Food Industry**: Sauces, soups, oils, and condiments are frequently packaged in sachets for easy use and storage.
- **Beverage Industry**: Liquid sachets for drinks like juices, energy drinks, and flavored waters cater to consumer preference for convenience.
- **Cosmetics and Personal Care**: Sachets for shampoos, conditioners, and lotions provide single-use options that appeal to consumers seeking portability.
- **Pharmaceuticals**: Liquid medications in sachets offer precise dosing and user-friendly packaging.
The adaptability of liquid sachet packing machines makes them a valuable asset across various sectors.
Technology Advancements in Liquid Sachet Packing
The evolution of technology has led to significant advancements in liquid sachet packing machines. Innovations in automation, software integration, and machine design have resulted in smarter, more efficient packing solutions. Key advancements include:
- **Smart Controls**: Modern machines feature advanced control systems that allow for real-time monitoring and adjustments, optimizing production speeds and minimizing downtime.
- **User-Friendly Interfaces**: Touchscreen controls make operation more intuitive, enabling quick training for operators.
- **Integration with Supply Chain Systems**: Machines can now integrate with inventory and supply chain management software, providing businesses with data that enhances operational planning.
These technological improvements ensure that liquid sachet packing machines remain at the forefront of packaging solutions.
Sustainability Considerations
In today’s business landscape, sustainability is a crucial factor. Liquid sachet packing machines can contribute to sustainable practices in several ways:
- **Reduced Packaging Waste**: The use of sachets minimizes material waste compared to traditional packaging methods.
- **Recyclable Materials**: Many sachets can be made from recyclable materials, aligning with eco-friendly initiatives.
- **Efficiency in Resource Use**: Machines designed for optimal energy consumption can lead to lower carbon footprints in production environments.
By adopting liquid sachet packing technology, companies can enhance their sustainability efforts, appealing to environmentally conscious consumers.
Choosing the Right Liquid Sachet Packing Machine
Selecting the right liquid sachet packing machine is critical to maximizing benefits. When considering a machine, businesses should evaluate the following factors:
- **Production Volume**: Assess the machine's capacity to ensure it meets your production demands.
- **Product Specifications**: Different liquids may require specific machine features, such as viscosity control or specialized filling nozzles.
- **Budget Considerations**: Balance the initial investment with long-term savings to choose a machine that fits your financial plans.
- **After-Sales Support**: Opt for suppliers that offer comprehensive support and maintenance services, ensuring your machine operates smoothly over time.
By carefully weighing these factors, businesses can make informed decisions that enhance their packaging operations.
FAQs About Liquid Sachet Packing Machines
1. What types of liquids can be packed using sachet machines?
Liquid sachet packing machines can handle a wide range of liquids, including sauces, oils, beverages, and even viscous products like creams.
2. What are the average production speeds of liquid sachet packing machines?
Depending on the model, these machines can produce anywhere from 30 to over 300 sachets per minute.
3. Are liquid sachet packing machines suitable for small businesses?
Yes, many models are designed to accommodate various production scales, making them suitable for both small and large operations.
4. How does the sealing process work in these machines?
The sealing process involves heating the edges of the sachet material to create an airtight seal, ensuring product freshness.
5. Can I customize the size and shape of sachets?
Most machines offer customization options for sachet size and shape, allowing businesses to align with branding requirements and consumer preferences.
Conclusion
Liquid sachet packing machines represent a significant advancement in the packaging industry, offering compelling advantages such as increased efficiency, cost-effectiveness, and enhanced product integrity. Their versatility allows them to cater to a variety of applications across multiple sectors, making them a valuable investment for businesses aiming to optimize their packaging processes. As technology continues to advance, these machines will likely play an even more crucial role in meeting the evolving demands of the marketplace. By understanding the benefits and making informed decisions regarding machine selection, businesses can position themselves for success in a competitive landscape.
liquid sachet packing machine

Innovations in Granule Packing Technology You Should Know
Innovations in Granule Packing Technology: A Comprehensive Guide Table of Contents Understanding Granule Packing Technology Importance of Granule Packing in Manufacturing Key Innovations in Granule Packing Technology The Role of Automation in Granule Packing Sustainable Packaging Solutions for Granules Advanced Sensors and Monitoring Systems Case Studies and Industry Examples Futu
2026-08-28
Maximize Efficiency with Advanced Tea Bag Packing Machines
In the realm of packaging machinery, tea bag packing machines represent a vital innovation for manufacturers in the tea industry. These specialized machines are designed to automate the tea bag production process, significantly increasing efficiency while maintaining the quality of the product. With the growing demand for convenient tea options, understanding the functionality and advantages of te
2026-08-27
How Food Packaging Machines Enhance Product Safety and Compliance
How Food Packaging Machines Enhance Product Safety and Compliance Table of Contents 1. Introduction to Food Packaging Machines 2. The Importance of Food Safety in Packaging 3. Types of Food Packaging Machines 4. Advanced Technologies in Food Packaging 5. Regulatory Compliance in Food Packaging 6. The Impact of Food Packaging on Product Safety 7. Best Practices for Food
2026-08-26

Head office :
112 ROBINSON ROAD #03-01 ROBINSON 112 ,SINGAPORE
HONGKONG BRANCH :
12/F ZJ 300 300 LOCKHART ROAD WAN
CHAI HK
GUANGZHOU BRANCH:
3th, Yilongjie Wulonggang, Zhongluotan, Baiyun district, Guangzhou,China
Subscribe to our newsletter and get professional packaging solution


SAF Coolest v1.3.1.2 设置面板 UFQSX-ANRV-PSSVE-XVF
无数据提示
Sorry, the current column is being updated, please look forward to it!